Main Menu
Hot extrusion is moving from a specialist process to a strategic capability for aluminum, copper, and advanced alloy production. The International Aluminium Institute projects global aluminum demand could reach 119.5 million tonnes by 2050, compared with 86.2 million tonnes in 2020. That growth increases pressure on manufacturers to deliver stable, energy-efficient, and serviceable equipment.
A Hot Extrusion Hydraulic Press Line must do more than generate force. It must control billet temperature, ram speed, container alignment, lubrication, cooling, and cycle consistency. A small temperature deviation can produce surface tearing, dimensional variation, or costly billet waste. The U.S. Department of Energy also identifies industrial process efficiency as a major opportunity for reducing manufacturing energy consumption. This makes hydraulic efficiency and heat recovery important evaluation points.
Professor Taylan Altan, a respected authority in metal forming, emphasized, “The quality of the product depends on controlling the forming process.” That principle guides this manufacturer review. It also prevents a common mistake: judging presses by tonnage alone.
No ranking is perfect.
The seven companies discussed here are compared through practical criteria, including press capacity, extrusion speed, automation, maintenance access, safety design, commissioning support, and proven installations. Data from Grand View Research, the International Aluminium Institute, and published manufacturer specifications provide useful market context, but specifications can differ between regions and project conditions. Buyers should verify references, energy consumption, spare-parts response, and actual output before signing a contract. The strongest Hot Extrusion Hydraulic Press Line is not always the largest. It is the line that performs reliably beside a real production furnace, shift after shift.
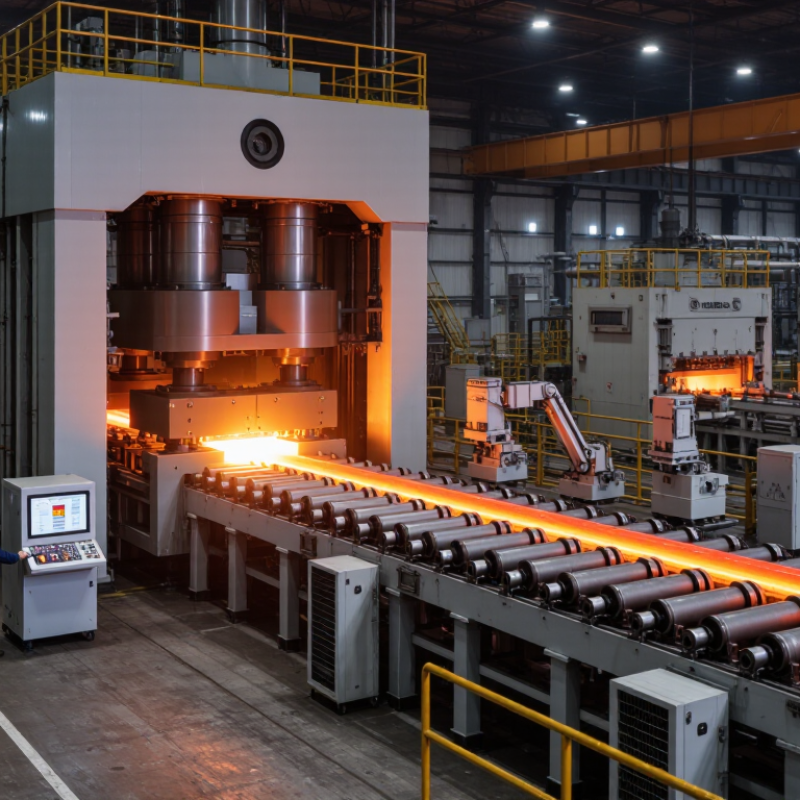
The seven strongest manufacturers in this field usually offer equipment from 250 to 10,000 tons. Capacity must match billet diameter, alloy strength, profile size, and expected production volume. A small 250-ton line may suit precision aluminum profiles, while heavy sections can require several thousand tons. Oversizing the press can increase energy use and reduce operating flexibility.
Working temperatures between 400 and 500°C demand careful thermal control. The billet furnace should maintain even heating across its length. Die preheating also matters, because sudden temperature differences can cause surface defects or premature tool wear. Experienced suppliers provide closed-loop temperature sensors, adjustable ram speed, and pressure monitoring. These features help operators identify unstable extrusion conditions before scrap increases.
During factory inspections, I would check frame stiffness, hydraulic response, alignment accuracy, and maintenance access. A reliable line should include guarded tooling areas, emergency controls, and clear operating records. Remote diagnostics can reduce downtime, but they do not replace skilled technicians. I would not assume that the highest tonnage means better performance. In practice, poor die design or uneven heating can undermine an otherwise powerful press. Ask each manufacturer for verified test data, sample profiles, energy figures, and references from comparable applications. Small details matter.
Choosing among the 7 best hot extrusion hydraulic press line manufacturers requires more than comparing catalog prices. Press force is the starting point. It must match billet material, diameter, temperature, and target profile. Oversized equipment can waste energy and floor space. Undersized equipment may produce unstable extrusion and premature component wear.
Ram speed affects productivity and surface quality. Look for adjustable speed profiles, not only a high maximum figure. A controlled approach speed can reduce impact, while steady extrusion speed supports consistent dimensions. Accuracy also matters. Check frame rigidity, pressure stability, die alignment, and repeatability across long production runs. Ask for measured tolerances, maintenance records, and factory acceptance test data. Marketing claims are not enough.
Energy use deserves practical attention. Compare installed power with actual consumption per billet, including heating, hydraulics, cooling, and idle periods. Variable-speed pumps and heat recovery can lower operating costs, but savings depend on real production conditions. Some specifications look impressive until tested under full load.
Tips: Request a sample extrusion trial using your alloy and billet size. Record force, ram speed, cycle time, temperature variation, and electricity use. Leave room for doubt. Supplier data may reflect ideal settings, not daily production. A site visit and operator interview can reveal weaknesses that brochures never mention.
Anonymous engineering benchmark comparison based on press force, extrusion ram speed, positioning accuracy, and press-line electricity use.
The chart uses a relative performance index from 0 to 100 to compare different engineering priorities. Tooltips show the underlying reference values: press force in MN, ram speed in mm/s, positioning accuracy in mm, and electricity consumption in kWh per tonne of extruded product. Lower energy use and smaller accuracy deviation indicate better performance. Values represent anonymous reference configurations and exclude billet-heating energy.
Seven Leading Hot Extrusion Hydraulic Press Line Manufacturers
The seven leading hot extrusion hydraulic press line manufacturers compete through force control, billet heating, and dependable automation. A reliable line should maintain stable pressure during piercing, extrusion, cooling, and cut-off operations. Operators notice weak systems quickly. Surface cracks, uneven wall thickness, and delayed cycle times often reveal poor coordination.
The International Aluminium Institute reported global primary aluminium production above 70 million tonnes in 2023. That volume supports continuing investment in efficient extrusion equipment. Grand View Research also identifies energy efficiency and automated control as major trends in the industrial hydraulic press market. These findings make servo-hydraulic drives, heat recovery, and real-time pressure monitoring important evaluation points.
Experienced buyers should compare the seven manufacturers by installed capacity, commissioning records, and after-sales response. A 10,000-ton line may suit heavy profiles, while smaller systems can reduce energy use for specialized components. Ask for measured cycle data, not attractive estimates. ISO 9001 certification helps, but it does not guarantee practical performance. I have found that maintenance access is often underestimated. Technicians need clear access to valves, pumps, heaters, and sensors. Otherwise, a minor seal failure can stop production for hours. Forecasts can be imperfect, too. Actual results depend on alloy grade, billet temperature, tooling design, and operator skill.
| Rank | Manufacturer Profile | Primary Production Region | Typical Press-Force Range | Common Hot-Extrusion Applications | Press Configuration | Automation Capability | Typical Billet Diameter Range | Applicable Quality Standards | Key Selection Strength |
|---|---|---|---|---|---|---|---|---|---|
| 1 | Manufacturer A | Western Europe | 10,000–80,000 kN | Aluminum profiles, copper tubes, brass sections, and industrial components | Four-column or prestressed-frame hydraulic press line | High Integrated billet heating, loading, extrusion, and run-out control | 150–500 mm | CE-oriented design; ISO 9001 quality systems commonly available | High engineering integration and customized turnkey lines |
| 2 | Manufacturer B | Central Europe | 12,000–65,000 kN | Aluminum automotive profiles, copper alloys, and precision sections | Direct-extrusion hydraulic press with independent container and dummy-block control | High PLC, HMI, recipe management, and production-data monitoring | 180–450 mm | ISO 9001-based manufacturing; CE conformity available for applicable markets | Accurate process control and repeatable product quality |
| 3 | Manufacturer C | East Asia | 8,000–50,000 kN | Aluminum profiles, copper rods, brass bars, and non-ferrous alloy products | Horizontal direct-extrusion press with modular auxiliary equipment | Medium to High Automatic billet transfer and programmable press cycles | 120–400 mm | ISO 9001 production management; export configurations can include CE documentation | Broad configuration options and competitive project cost |
| 4 | Manufacturer D | North America | 10,000–45,000 kN | Aluminum extrusion, copper and brass products, and heavy industrial sections | Heavy-duty hydraulic press with separate heating and cooling systems | Medium Automated press sequencing with optional robotic handling | 150–350 mm | ANSI, ASME, OSHA, and customer-specific safety requirements may be supported | Robust construction and strong after-sales service capability |
| 5 | Manufacturer E | Southern Europe | 6,000–35,000 kN | Medium-size aluminum profiles, copper tubes, and specialized alloy sections | Compact horizontal press line with integrated billet and profile handling | Medium to High Automatic loading, cut-length control, and production alarms | 100–300 mm | CE marking support and ISO 9001-based quality procedures | Space-efficient layouts and flexible mid-range production |
| 6 | Manufacturer F | East Asia | 5,000–30,000 kN | Aluminum architectural profiles, copper products, and general-purpose sections | Standardized direct-extrusion hydraulic press with optional auxiliary modules | Medium Automatic billet feed and programmable hydraulic control | 90–280 mm | ISO 9001 manufacturing practices; regional electrical and safety compliance available | Shorter delivery options and economical standard configurations |
| 7 | Manufacturer G | South Asia | 4,000–25,000 kN | Aluminum profiles, copper rods, brass sections, and small-batch production | Compact hydraulic press line with separately specified heating and run-out units | Basic to Medium PLC-based sequencing with optional automatic material handling | 80–250 mm | ISO 9001-oriented production; compliance documentation depends on project destination | Accessible maintenance, practical customization, and lower entry cost |
Note: The specifications shown are representative market ranges for hot extrusion hydraulic press lines. Final press force, billet diameter, automation level, safety certification, and auxiliary equipment should be confirmed against the supplier’s current technical proposal.
Choosing among the 7 best hot extrusion hydraulic press line manufacturers requires more than comparing headline tonnage.
Billet size is the practical starting point. A press handling 6-inch billets may suit standard aluminum profiles, while larger billets support heavier sections and higher output. Check the container diameter, maximum extrusion length, and loading method. These details affect die changes, heating time, and floor space.
Alloy range also matters. Aluminum alloys behave differently under pressure and temperature. A capable line should maintain stable billet heating, controlled ram speed, and accurate pressure feedback. Ask for production records using your target alloys, not generic samples.
Press ratings need careful reading. A 2,000-ton rating does not guarantee equal performance across every profile. Review rated force, working pressure, stroke length, and cycle speed together.
Automation separates a convenient line from a costly bottleneck. Look for automatic billet loading, die handling, quenching, puller control, and defect alarms. Data logging helps operators trace temperature drift or uneven profiles.
Factory acceptance testing is valuable, especially when it uses your billet dimensions and alloy recipe. Service response should include spare-part availability and technician training. I would not trust a polished brochure alone. Some published capacity figures assume ideal billets, experienced operators, and unusually short changeovers. Those assumptions deserve questions. A quieter test run may reveal more than a dramatic sales demonstration.
Choosing among the seven leading manufacturers requires more than comparing press capacity. Ask for a current ISO 9001 certificate and verify its scope. It should cover engineering, manufacturing, testing, and after-sales support. A factory visit can reveal practical details, such as machining accuracy, weld quality, and hydraulic cleanliness. Request references from plants using similar alloys, billet sizes, and production speeds.
Service coverage often determines whether a line performs reliably after installation. Check for trained local technicians, remote diagnostics, spare-parts availability, and clear response times. Ask who will supervise commissioning and operator training. A strong supplier should provide test records, maintenance schedules, and documented safety procedures. However, impressive documentation does not always guarantee fast field support. That point deserves careful questioning.
Lead time should include design approval, tooling, factory testing, shipment, installation, and production acceptance. Request a milestone schedule with realistic penalties for avoidable delays. Cost comparisons must include heaters, dies, automation, freight, installation, and future maintenance. The lowest quotation may exclude essential items. It may also use cheaper valves or control components. Review the five-year ownership cost, not only the purchase price. My own selection mistake would be trusting a polished presentation before checking replacement-part delivery times. That small oversight can stop an entire line.
Office: (281) 855-2218
Copyright © 2025 Telco Intercontinental Corp. All rights reserved. Privacy Policy | Legal Disclaimer
Telco®, TelcoMotion®, and TelcoGreen® are registered trademarks of Telco Intercontinental Corp.